Home
3D
PrintUP 3D Printer
PioCreat 3D Printer
Printers
FastCOLOUR >>
ATools
DTF Textile
UV-DTF
FlatPRINT
PrintExp
InkRIP
Lasers
TruCUT CO
2
>>
TruCUT RDWorks
TruCUT 2020+
TruCUT Express
TruCUT Lite >>
4030 & Vertical Software
4030 & Vertical Documents
New 6040 Desktop
LabelMark
RayCUT
MorCUT >>
MorCUT-Cyclops
LaserMaster
Plasmas
MetalWise
Fabricam
Routers
EasyRoute
PowerRoute
Blade Cutters
Vinyl Cutters >>
V-Series
V-Smart
V-Auto (& V-Smart+)
Vinyl4
Flatbed Cutters >>
FlatCUT
Label Cutters >>
V-Auto Label Cutters
Software >>
VinylCut
More
FastCUT
Heatware
Rollman
ScreenMaster
Other Software
Miscellaneous
AM.CO.ZA
/
Buy CNC Software
/
CNC Software Training
/
CNC Software Downloads
Sales: 072 222 2211
Support: 076 666 6655
Training: 060 818 1818
Jo’burg: 087 802 5368
Cape Town: 087 802 7106
An
Project
Multimedia
Univision Videos
#SortIT Videos
MakersLab.TV
Software Training
Welldone Gallery
Updates
Prevision Blog
Cornerstone Trust
Email Campaigns
Contact Us
Sales WhatsApp
060 600 6000
Support WhatsApp
060 600 7000
Johannesburg Headquarters
011 397 1429
087 802 5368
Cape Town Showroom
021 555 3250
087 802 7106
Links
CNC Machine Repair
Vinyl Cutter
Heatware
You are here:
AM.CO.ZA
Buythis
CNC Utilities Homepage
MetalWise-CNC-Plasma-Cutting-Machine
MetalWise Lite Controller Parameters.pdf
Page 3 of 3
Page 3 / 147 of MetalWise Lite Controller Parameters
Home
3D
PrintUP 3D Printer
PioCreat 3D Printer
Printers
FastCOLOUR >>
ATools
DTF Textile
UV-DTF
FlatPRINT
PrintExp
InkRIP
Lasers
TruCUT CO
2
>>
TruCUT RDWorks
TruCUT 2020+
TruCUT Express
TruCUT Lite >>
4030 & Vertical Software
4030 & Vertical Documents
New 6040 Desktop
LabelMark
RayCUT
MorCUT >>
MorCUT-Cyclops
LaserMaster
Plasmas
MetalWise
Fabricam
Routers
EasyRoute
PowerRoute
Blade Cutters
Vinyl Cutters >>
V-Series
V-Smart
V-Auto (& V-Smart+)
Vinyl4
Flatbed Cutters >>
FlatCUT
Label Cutters >>
V-Auto Label Cutters
Software >>
VinylCut
More
FastCUT
Heatware
Rollman
ScreenMaster
Other Software
Miscellaneous
AM.CO.ZA
/
Buy CNC Software
/
CNC Software Training
/
CNC Software Downloads
Sales: 072 222 2211
Support: 076 666 6655
Training: 060 818 1818
Jo’burg: 087 802 5368
Cape Town: 087 802 7106
An
Project
Multimedia
Univision Videos
#SortIT Videos
MakersLab.TV
Software Training
Welldone Gallery
Updates
Prevision Blog
Cornerstone Trust
Email Campaigns
Contact Us
Sales WhatsApp
060 600 6000
Support WhatsApp
060 600 7000
Johannesburg Headquarters
011 397 1429
087 802 5368
Cape Town Showroom
021 555 3250
087 802 7106
Links
CNC Machine Repair
Vinyl Cutter
Heatware
You are here:
AM.CO.ZA
Buythis
CNC Utilities Homepage
MetalWise-CNC-Plasma-Cutting-Machine
MetalWise Lite Controller Parameters.pdf
Page 3 of 3
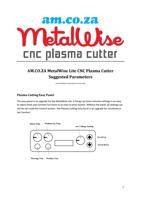
1
A
M.C
O
.Z
A
Metal
W
is
e
L
it
e
C
NC
Plasm
a C
u
tt
er
Sug
ge
s
te
d
Par
amet
er
s
L
a
t
e
s
t
M
o
d
if
ie
d
a
t
2
0
1
7
/
0
2
/
1
4
0
1
:
3
9
:
4
2
A
M
Pla
sm
a
C
u
t
t
i
n
g
E
a
sy
Pa
n
e
l
T
he
e
a
s
y
pa
n
e
l
i
s
a
n
up
gra
de
f
or
t
he
M
e
t
a
l
Wi
s
e
Li
t
e
.
It
bri
ng
s
up
s
ome
c
ommon
s
e
t
t
i
ng
s
i
n
a
n
e
a
s
y
t
o
a
djus
t
knob
a
nd
c
ommon
f
un
c
t
i
ons
t
o
a
n
e
a
s
y
t
o
pre
s
s
bu
t
t
on.
Wi
t
hou
t
t
he
pa
ne
l
,
a
l
l
s
e
t
t
i
ng
s
c
a
n
s
t
i
l
l
be
s
e
t
i
ns
i
de
t
he
C
on
t
r
ol
S
ys
t
e
m.
T
he
P
l
a
s
ma
C
ut
t
i
ng
Ea
s
y
P
a
n
e
l
i
s
a
n
up
gra
de
f
or
c
onv
e
ni
e
nce
not
f
un
c
t
i
on.
Pie
rc
e
T
im
e
P
o
s
i
ti
o
n
U
p
T
i
m
e
A
rc
-
V
o
l
ta
g
e
Setti
n
g
P
i
erci
n
g
Tes
t
P
o
s
i
ti
o
n
Tes
t
To
rch
U
p
To
rch
D
o
w
n
2
F1
C
omm
on
:
C
omm
on
S
e
t
t
i
n
g
s f
or
Pla
sm
a
a
n
d
Fla
me
C
u
t
t
i
n
g
S
e
t
t
i
ng
S
ug
ge
s
t
V
a
l
ue
Ma
x
C
ut
t
i
ng
S
pe
e
d
S
e
t
up
m
a
x
i
mu
m
c
ut
t
i
ng
s
pe
e
d
de
pe
nd
s
on
m
a
t
e
r
i
a
l
,
not
s
ug
ge
s
t
hi
gh
e
r
t
ha
n
40
00
mm/mi
n,
norma
l
l
y
30
0
–
20
00
mm/
mi
n
Ma
nu
a
l
Move
S
pe
e
d
60
00
m
m
/
m
i
n
,
6m
e
t
e
r
pe
r
mi
nu
t
e
i
s
t
he
ma
x
i
mu
m
s
pe
e
d
ma
c
hi
ne
de
s
i
gn
e
d
f
or
w
i
t
h
t
h
e
s
t
e
pp
e
r
mo
t
or
s
i
ns
t
a
l
l
e
d
G
00
Move
S
pe
e
d
40
00
m
m
/
m
i
n
,
t
he
t
or
c
h
mov
i
ng
s
pe
e
d
f
r
om
one
pa
t
h
t
o
a
not
he
r
w
i
t
hi
n
a
c
ut
t
i
ng
proc
e
s
s
.
S
e
t
l
ow
e
r
t
h
a
n
ma
x
i
mu
m
s
pe
e
d
a
voi
ds
l
oos
i
ng
s
t
e
ps
.
D
e
mo/Ba
c
k
S
pe
e
d
20
00
m
m
/
m
i
n
,
t
he
s
pe
e
d
us
e
d
f
or
mov
e
ba
c
k
w
a
r
ds
Ma
r
ke
r
S
pe
e
d
0,
no
us
e
K
e
r
f
V
a
l
ue
N
or
ma
l
l
y
0.
3
t
o
1m
m,
ha
l
f
of
t
he
va
l
ue
of
t
he
w
i
dt
h
of
t
he
c
u
t
t
i
ng
ga
p
C
or
ne
r
S
pe
e
d
9
5
%
of
norma
l
s
pe
e
d
s
ug
ge
s
t
e
d,
c
a
n
be
l
ow
e
r
i
f
not
c
u
t
t
i
ng
t
h
r
oug
h
D
e
mo
Ru
n
S
pe
e
d
40
00
m
m
/
m
i
n
,
t
he
s
pe
e
d
us
e
d
f
or
de
mon
s
t
r
a
t
i
on
c
ut
t
i
ng
proc
e
s
s
C
ut
t
i
ng
T
yp
e
F
l
a
me
,
P
l
a
s
m
a
or
D
e
mo
,
de
p
e
nd
s
on
you
r
r
e
q
ui
r
e
me
nt
F
3
Pla
sm
a
:
Pla
sm
a
C
u
t
t
i
n
g
S
e
t
t
i
n
g
s
#
t
hos
e
v
a
l
ue
s
ha
ve
b
e
e
n
ov
e
r
r
i
de
by
t
he
Ea
s
y
P
a
ne
l
S
e
t
t
i
ng
S
ug
ge
s
t
V
a
l
ue
D
e
l
a
y
Be
f
or
e
Arc
0.
3
–
0.
4s
,
t
i
me
de
l
a
y
f
r
om
t
o
r
c
h
pos
i
t
i
one
d
t
o
a
r
c
,
t
o
a
voi
d
vi
bra
t
i
on
P
i
e
r
c
e
T
i
me
#
0.
3
–
0.
8s
or
mor
e
,
de
pe
nd
s
on
t
he
pl
a
t
e
t
hi
c
kne
s
s
T
or
c
h
U
p
T
i
me
1
–
2
s
,
w
h
e
n
f
i
ni
s
h
one
c
ut
,
l
i
f
t
t
i
me
be
f
or
e
m
ove
t
o
ne
x
t
on
e
Arc
i
ng
C
he
c
k
T
i
me
1
5
s
P
os
i
t
i
on
C
he
c
k
T
i
me
#
1
0
s
P
os
i
t
i
on
U
p
T
i
me
#
0.
3
–
0.
6s
,
a
f
t
e
r
t
or
c
h
t
ou
c
he
d
pl
a
t
e
,
l
i
f
t
t
i
me
be
f
or
e
pos
i
t
i
one
d
a
nd
a
r
c
.
T
he
opt
i
ma
l
di
s
t
a
nce
f
or
pi
e
r
c
i
ng
i
s
be
t
w
e
e
n
2
-
3
mm
.
S
pe
e
d
t
o
Loc
k
T
H
C
95
.
00
%
mm/mi
n,
di
s
a
bl
e
T
H
C
i
f
s
pe
e
d
l
ow
e
r
t
ha
n
t
hi
s
s
e
t
t
i
ng
D
i
s
t
a
nce
t
o
Loc
k
T
H
C
5m
m
,
w
he
n
pa
r
t
of
c
ut
t
i
ng
pa
t
h
l
e
s
s
t
ha
n
t
hi
s
di
s
t
a
nce
,
di
s
a
bl
e
T
H
C
Los
e
Arc
D
e
l
a
y
0
s
,
de
l
a
y
f
or
ma
c
hi
ne
gi
ve
s
w
a
r
ni
ng
w
he
n
a
r
c
broke
.
N
e
e
d
t
o
s
e
t
up
de
l
a
y
i
f
you
c
ut
me
s
h
or
gri
l
l
,
or
w
i
t
h
l
e
a
d
i
n/
out
-
-
t
r
y
0.
5s
.
F
or
H
yp
e
r
t
he
r
m
un
i
t
,
t
r
y
1.
5s
s
i
nce
t
he
s
i
gn
a
l
f
r
om
H
yp
e
r
t
h
e
r
m
P
ow
e
r
m
a
x
un
i
t
ge
n
e
r
a
l
l
y
ha
ve
de
l
a
ys
.
T
i
me
t
o
Loc
k
T
H
C
Be
f
or
e
M08
0
s
Wa
t
c
h
Ar
c
En
a
bl
e
Y
e
s
,
e
na
bl
e
Arc
-
V
ol
t
a
g
e
c
h
e
c
ki
ng
.
S
e
t
t
o
N
o
t
o
di
s
a
bl
e
T
H
C
U
s
e
C
yl
i
nd
e
r
T
H
C
N
o
A
r
c
-
V
o
l
t
a
g
e
#
1
3
0
.
0
0
V
C
ha
ng
e
t
he
va
l
ue
t
o
ge
t
opt
i
ma
l
di
s
t
a
nce
of
c
ut
t
i
ng
be
t
w
e
e
n
pl
a
t
e
t
o
noz
z
l
e
a
bou
t
2
-
3
mm
.
Ov
e
r
-
Ar
c
P
rot
e
ct
i
o
n
#
3
0
.
0
0
V
Sen
s
i
t
i
v
e
#
4
0
.
0
0
%
St
e
p
#
1
.
0
0
V
P
o
s
i
t
i
o
n
T
i
m
e
#
6
.
0
0
S
3
F
5
S
y
st
e
m
:
S
y
st
e
m
S
e
t
t
i
n
g
s
S
e
t
t
i
ng
S
ug
ge
s
t
V
a
l
ue
H
or
i
z
ont
a
l
Ax
i
s
P
ul
s
e
V
e
r
t
i
c
a
l
Ax
i
s
P
ul
s
e
4
5
3
.
0
0
0
o
r
5
0
0
.
0
0
0
P
u
l
s
e
/
m
m
,
k
e
e
p
o
r
i
g
i
n
a
l
v
a
l
u
e
.
T
h
i
s
v
a
l
u
e
i
s
me
c
ha
ni
c
a
l
de
p
e
nd
a
nt
a
nd
us
e
t
o
de
t
e
r
mi
ne
di
s
t
a
nce
mov
e
d
Ma
x
C
ut
t
i
ng
S
pe
e
d
Ma
x
G
00
S
pe
e
d
Ma
x
Ma
nu
a
l
S
p
e
e
d
C
a
n
s
e
t
a
t
ma
c
hi
ne
ma
x
i
mu
m
pos
s
i
bl
e
s
pe
e
d
80
00
mm/mi
n,
bu
t
s
ug
ge
s
t
us
e
60
00
mm/mi
n
or
l
ow
e
r
.
S
ma
l
l
Arc
Li
mi
t
50
0m
m/
mi
n
Li
mi
t
e
d
S
pe
e
d
Be
l
ow
Ra
di
us
15
mm,
t
hi
s
s
e
t
t
i
ng
gi
ve
s
you
be
t
t
e
r
c
u
t
t
i
ng
q
ua
l
i
t
y
on
s
ma
l
l
c
i
r
c
l
e
s
.
Acc
e
l
e
r
a
t
e
T
i
me
i
n
F
l
a
me
0
.
4
0
s
Acc
e
l
e
r
a
t
e
T
i
me
i
n
P
l
a
s
ma
0
.
3
0
s
Em
e
r
ge
ncy
S
t
op
T
i
me
0
.
0
8
s
S
t
a
r
t
S
p
e
e
d
25
0m
m/
mi
n
Ma
x
+
X
Ma
x
+
Y
Mi
n
-
X
Mi
n
-
Y
Me
t
a
l
Wi
s
e
Li
t
e
doe
s
not
c
ome
w
i
t
h
l
i
mi
t
s
w
i
t
c
h,
t
he
mov
i
ng
di
s
t
a
nce
de
t
e
r
mi
ne
d
by
me
c
ha
ni
c
a
l
s
t
r
uct
ur
e
.
K
e
e
p
de
f
a
ul
t
s
e
t
t
i
ng
,
1
0
0
0
0
0
.
0
0
m
m
f
or
Ma
x
,
a
nd
-
1
0
0
0
0
0
.
0
0
m
m
f
o
r
M
i
n
.
"
Do you need help?
Call Me Back
"
Do you need help?
Call Me Back